Every module relies on its cover glass to block UV light, withstand hail, and let sunlight through. But even glass labeled the same way — "ultra-clear, patterned, tempered, AR-coated" — can differ by a wide margin in the yield and outdoor service life that different manufacturers actually deliver. That difference is rarely written in the specification sheet; it is hidden in the control of every single step of the manufacturing process.
For module manufacturers and procurement teams comparing suppliers and quotes, understanding these 8 steps is more useful than memorizing a transmittance number.
Ordinary float glass has a relatively high iron content and a greenish appearance; its visible-light transmittance is only about 88–90%, and it absorbs part of the spectrum that cells genuinely need. Under the national standard, 3.2mm non-coated ultra-clear patterned glass must achieve a photovoltaic transmittance of 91.5% or higher, and the requirement is even higher after coating (≥93.0%). As TOPCon, HJT, and perovskite–silicon tandem cells become increasingly sensitive to light transmission, low-iron ultra-clear glass has therefore become a hard prerequisite — ordinary float glass cannot meet this transmission threshold.
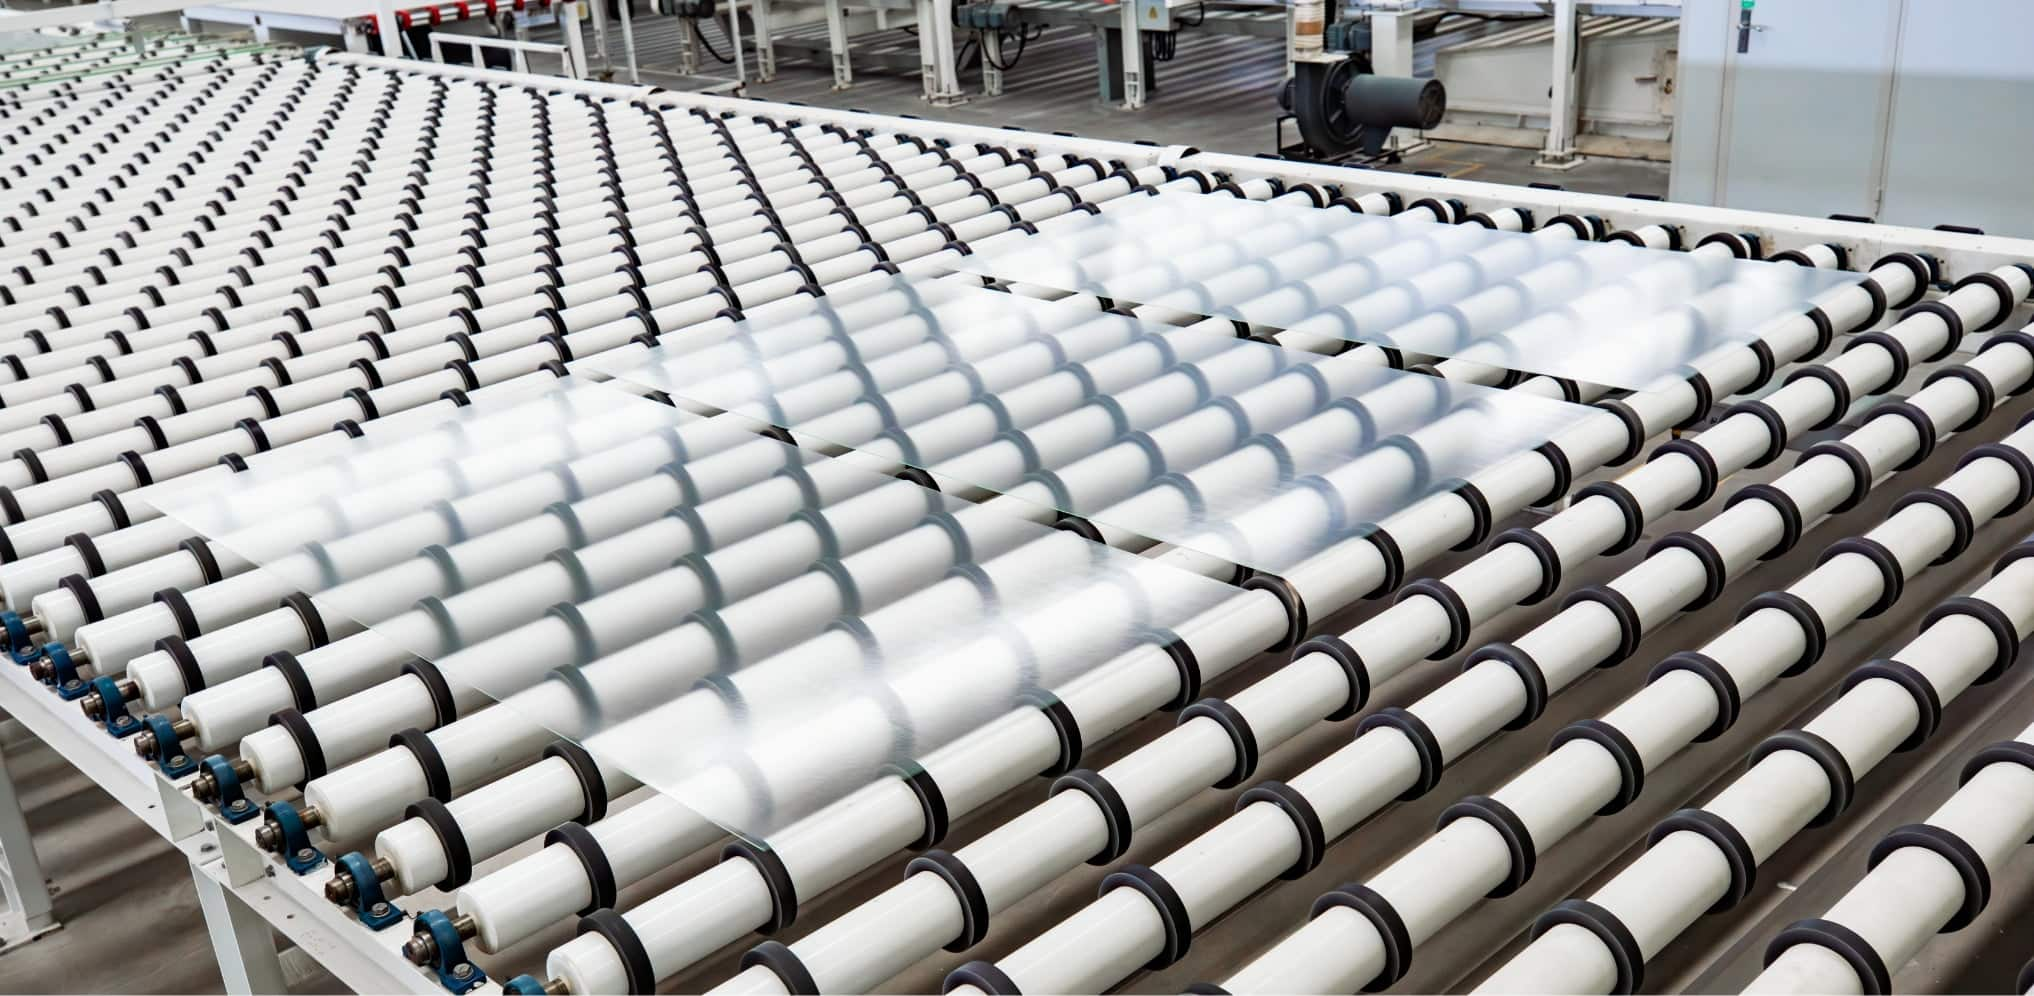
At the same time, the mainstream material for PV cover glass is ultra-clear rolled (patterned) glass, not float glass: the rolling roller presses a fine textured surface directly onto the molten glass, which both strengthens adhesion with the encapsulant film and aids anti-reflection. Float glass, with its extremely flat surface, is better suited to thin-film modules and BIPV curtain walls.
(1) Batching: Low-iron silica sand, soda ash, and dolomite are precisely mixed in set proportions. Iron content is the source of light transmission, and a batching deviation can directly eat away several percentage points of power generation.
(2) Melting: The batch enters a furnace at about 1580–1620°C, where it is homogenized, fined, and degassed of bubbles.
(3) Rolling and forming: Molten glass at about 1100°C passes through upper and lower counter-rotating rollers; the lower roller carries an engraved pattern, forming both the thickness and the textured surface in a single pass. Sheet thickness, pattern, and flatness are set here.
(4) Annealing: Slow cooling removes internal stress; glass that is not fully annealed is prone to spontaneous breakage later.
(5) Cutting: The glass is cut to module dimensions; the thinner the glass, the more prone it is to edge chipping and micro-cracks.
(6) Edge grinding: Grinds away the micro-cracks and edge chips left by cutting — this step directly determines downstream tempering yield and transport breakage rates.
(7) Tempering: The glass is heated to near its softening point and then rapidly air-quenched, creating a compressive stress layer on the surface that multiplies strength several times over and causes the glass to fracture into small granules when broken. Whether the stress distribution is uniform is the dividing line for tempering yield.
(8) AR coating: A porous silica film is deposited by magnetron sputtering or sol-gel, bringing surface reflectance down from about 8% to below 2% and raising transmittance by a further 2–4 percentage points.
Beyond the specification sheet, here are six points we recommend asking suppliers directly:
(1) Iron-content test reports on raw materials, and whether there is a stable, self-owned silica sand source;
(2) Daily melting capacity of the furnace, and its homogenization and combustion configuration;
(3) The online sampling-inspection ratio for bubbles, stones (inclusions), and roller marks on the sheet surface;
(4) Tempering yield and stress-uniformity data, rather than just "yes, we can temper";
(5) Full-size uniformity mapping of AR coating thickness, rather than a single-point transmittance reading;
(6) Which laboratory performed the coating weathering tests (damp heat, salt spray, abrasion).
When we make PV glass, the core is controlling each of these 8 steps consistently on a mass production line. The Beihai base in Guangxi operates 4 PV rolled-glass furnaces, each with a daily melting capacity of 1,200 tons; the silica sand raw material is supplied directly from the group’s nearby mining area in Shagang Town, Hepu County. Low-iron ultra-clear rolled substrates, tempering, vacuum magnetron AR coating, and enamel (frit) screen printing are all completed within the same industrial park — the glass goes from sand to finished sheet without leaving the site.
The yield of cover glass is never decided by any single number, but by the process consistency of every one of the 8 gates. If you are selecting cover glass for a module project, or would like to verify our real delivery capability in rolling, tempering, and coating, send us your specifications — our engineering team will provide process recommendations and sample solutions.
WhatsApp : +8615059190820
WhatsApp : +8618850736588
Email : elva@xfxglass.com
Email : business@xfxglass.com
Tel : +8615059190820
Tel : +8618850736588